
Detect deviations early and release deliveries with confidence

Quality control in Bulgaria: assurance before shipping

A deviation discovered only on receipt can disrupt production planning. For quality control in Bulgaria, TOS therefore focuses agreements on moments when correction is still possible: before the series, during critical operations and before shipping. Your drawings, functional requirements and acceptance criteria form the basis.

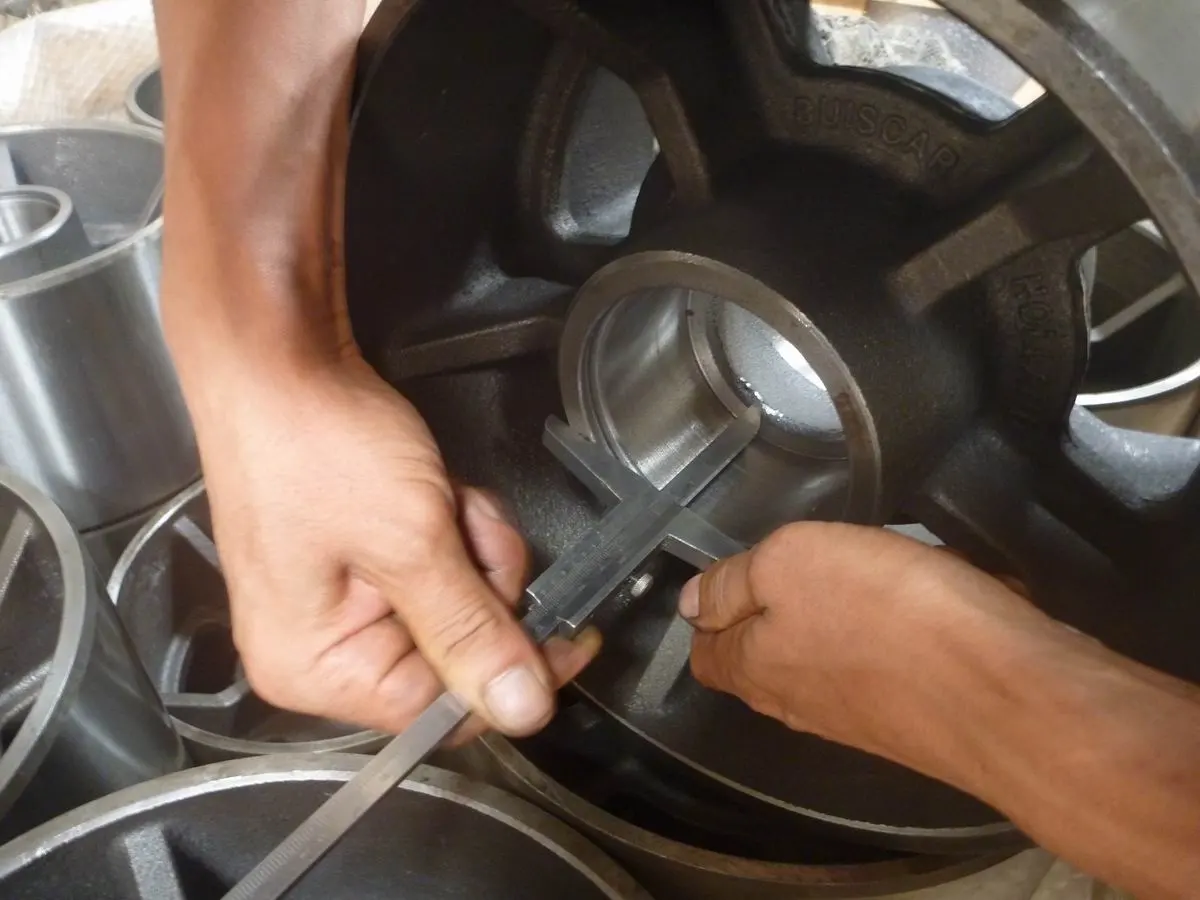
Boring van een gegoten machineonderdeel meten met een schuifmaat

Inspection agreements matched to your product

Define critical features

Focus attention on features that affect assembly, function and use.

Align the measurement method

Discuss suitable measuring equipment and references before production.

Enable timely correction

Plan inspection before rework becomes difficult or costly.

Report deviations

Define reporting timing, assessment and decision authority.

Release with purpose

Review results and delivery agreements together before shipping.
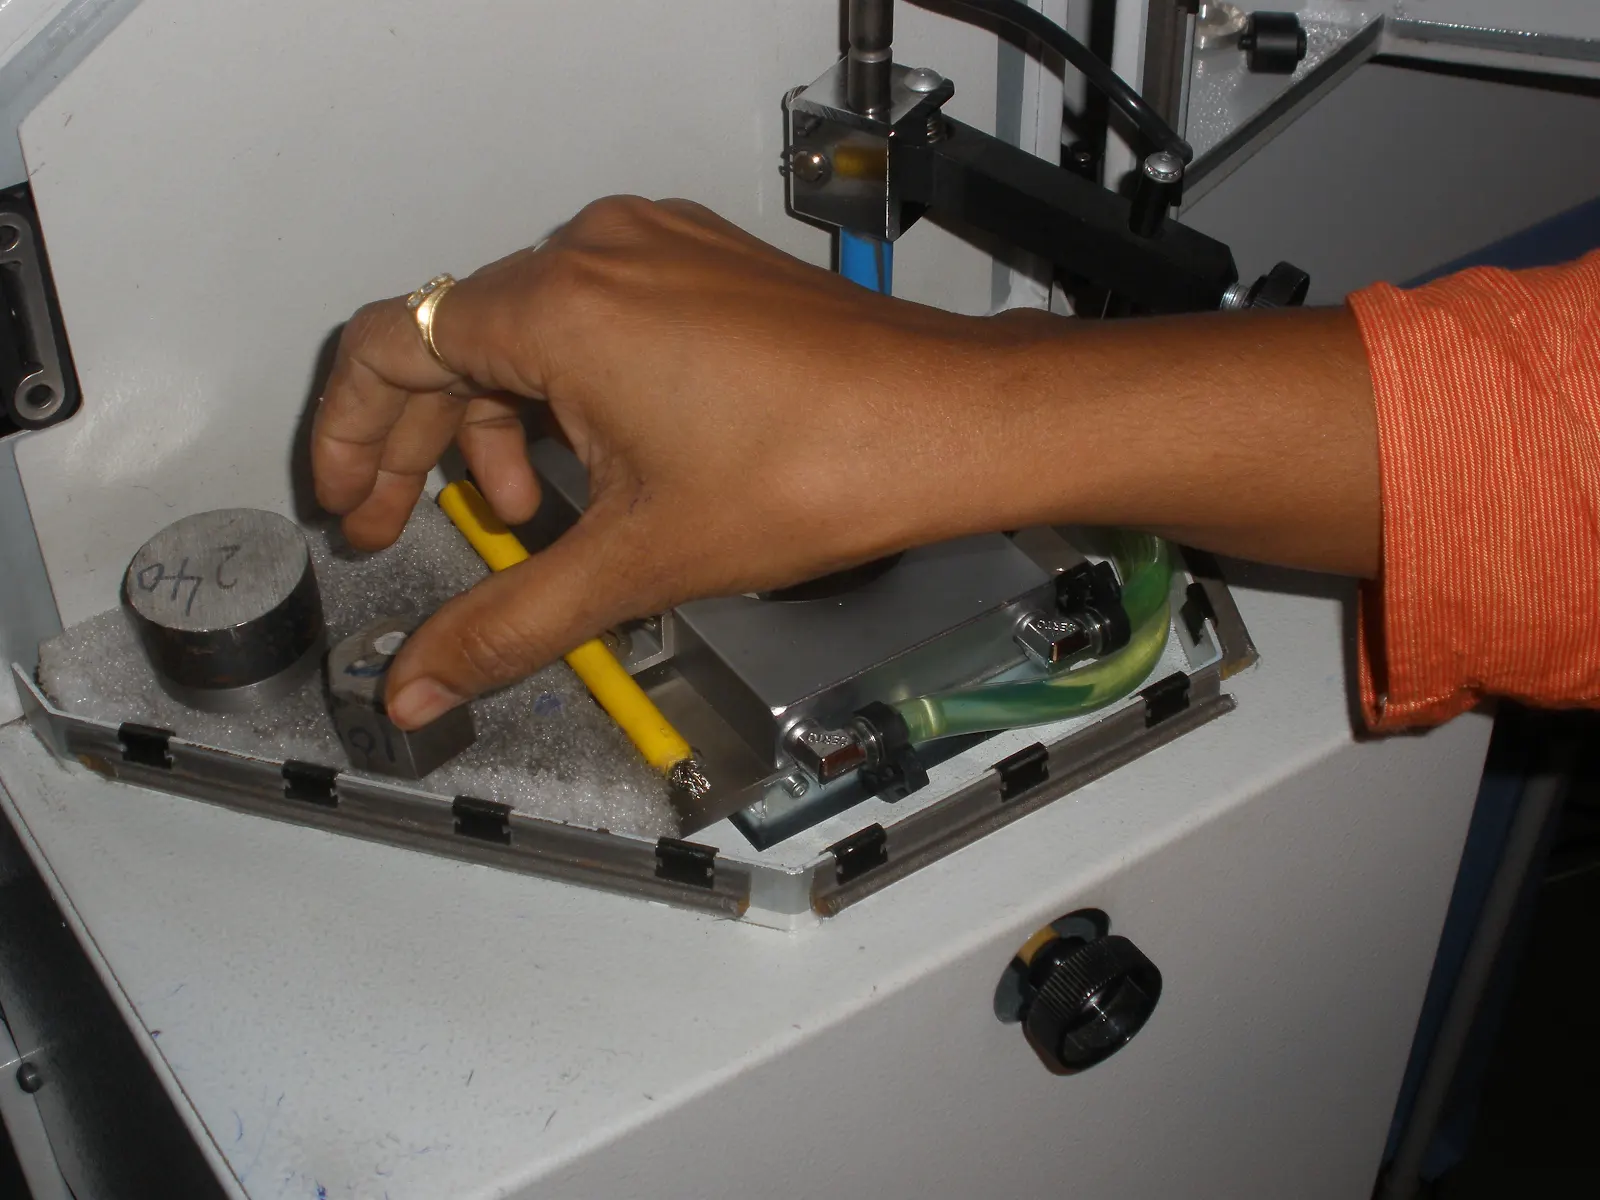
Metalen proefstuk positioneren bij een meetopstelling

Plan inspection before production starts

For manufacturing in Bulgaria, we define before production which features determine assembly, function or further processing. These may include interface dimensions, visible surfaces, material data or an agreed function. Your drawing and revision, together with concrete acceptance criteria, form the basis.

Measuring equipment, inspection frequency and reporting are aligned with the selected manufacturing partner. We choose inspection points where correction is still possible, for example before surface treatment or before an assembly is closed.

A deviation found only after delivery can cause rework, extra transport and downtime. The longer transport route from Bulgaria makes timely feedback especially important. We therefore agree when the partner reports a deviation, which information is required and who decides on the solution.

Lower processing cost does not change your quality requirements. When comparing Poland or China, the same product specifications remain authoritative. Transport distance, rework options and the desired presence at the manufacturer help determine the inspection approach. See our manufacturing locations for the broader comparison.

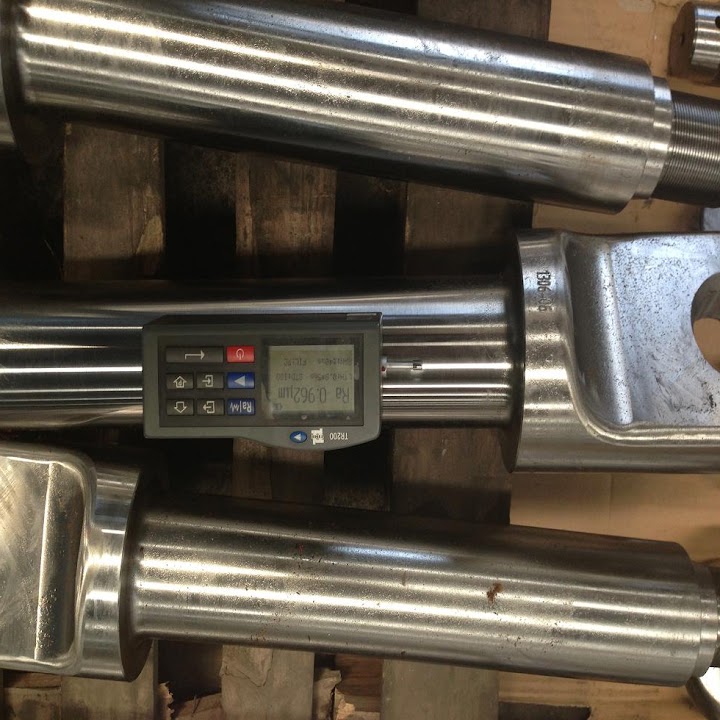
Ruwheidsmeter op de bewerkte schacht van een metalen trekoog

From product specification to release

1. Make requirements specific

Bring drawing, revision and acceptance criteria together.

2. Set up inspection

Agree measurement method, frequency and recording.

3. Verify the first build

Assess results before repeating the series.

4. Handle deviations

Align rework or the next step with the authorised party.

5. Release the delivery

Check product, completeness and protection.
From individual parts to complete assemblies

For CNC-milled parts, inspection may focus on critical dimensions and interfaces. For welded frames, form, interface dimensions and agreed weld features may be central. For sheet metal assemblies, hole patterns, bend dimensions and visible surfaces are among the features assessed.

For assembly in Bulgaria, completeness, fit and the agreed movement or function are added. A photo can clarify execution but does not by itself prove dimensional accuracy or material identity. Where evidence is needed, we agree suitable measurement or documentation.

Which features deserve extra attention?

Ten agreements for quality control in Bulgaria

A practical quality control approach connects product requirements with concrete inspection points. We define what the manufacturing partner checks, which results you receive and when the delivery can be released. The agreements below are tailored to your order.

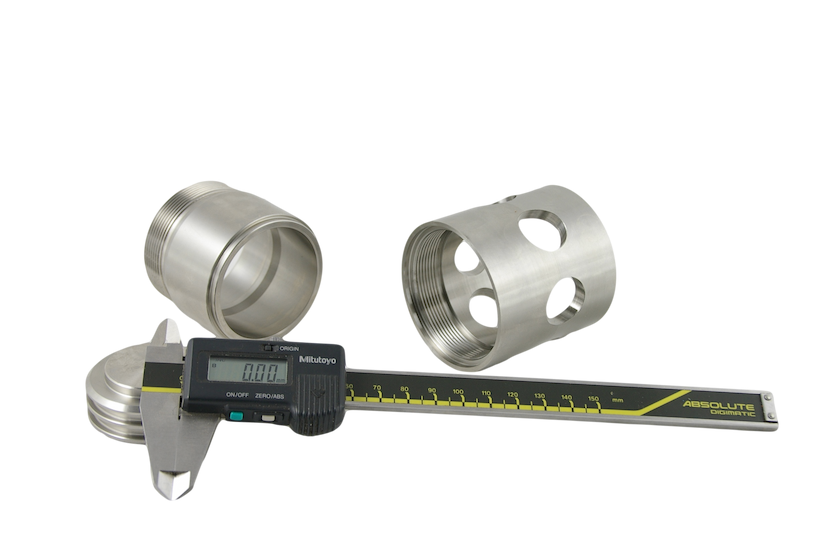
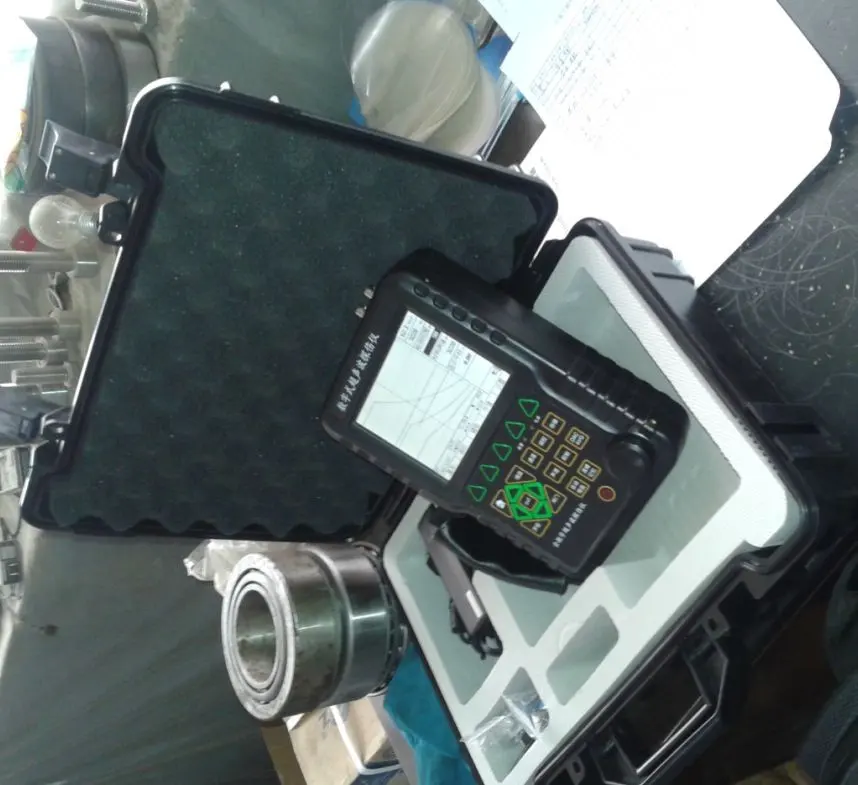
Draagbaar meetapparaat in een koffer naast bewerkte metalen onderdelen

Determine which features directly affect assembly, use or further processing. Link them to the authoritative drawing and revision.

Describe permitted deviations and how doubtful cases are handled. Define visual quality as concretely as possible.

Discuss accessibility, reference points and suitable measuring equipment. The required accuracy must be assessable with the selected method.

Agree when a first article or pilot series is required and who releases the result. Implement corrections before repetition.

Place inspection where an error can still be corrected, for example before finishing or before closing an assembly.

Define which results must be recorded, which batch or revision they are linked to and which data you receive.

Agree when production or shipment is held. Rework, replacement or acceptance of a deviation is aligned with the authorised party.

Verify the agreed features and completeness. Final inspection does not replace necessary in-process inspection of features that later become inaccessible.

Check that execution, quantities, marking and protection match the delivery. Prevent approved products from being damaged in transport.

Translate lessons and changes into new instructions. Assess whether a material, process or revision change requires renewed release.

Examples from our manufacturing projects

Precision Machining for the Cryogenic Industry

For a client in the cryogenics industry, we produce high-quality machined parts that must meet strict safety and temperature requirements.....

Complete Ground Storage Bunkers: From Metal Fabrication to Fully Installed and Ready-for-Use Systems

For a client in the agricultural and industrial sectors, we manufacture complete ground storage bunkers, constructed entirely of high-quality steel.....

Questions about quality control in Bulgaria

Is every part inspected completely?

That depends on the agreed requirements and risks. Full inspection or a defined sampling plan is set per feature. A complete dimensional inspection of every part is not promised automatically.

The required reporting is agreed in advance, including features, measurement method and identification. The manufacturer must be able to record the requested data in the agreed format.

The deviation is assessed according to the agreed reporting and release procedure. Rework, replacement or exceptional acceptance is not decided silently; the selected solution is aligned.

No. Your product specification remains authoritative. The practical arrangement of inspection, feedback and rework may differ because of the manufacturing route and transport distance.

Only when they are part of the order. Required documents, expertise and any external testing are confirmed for each product.