
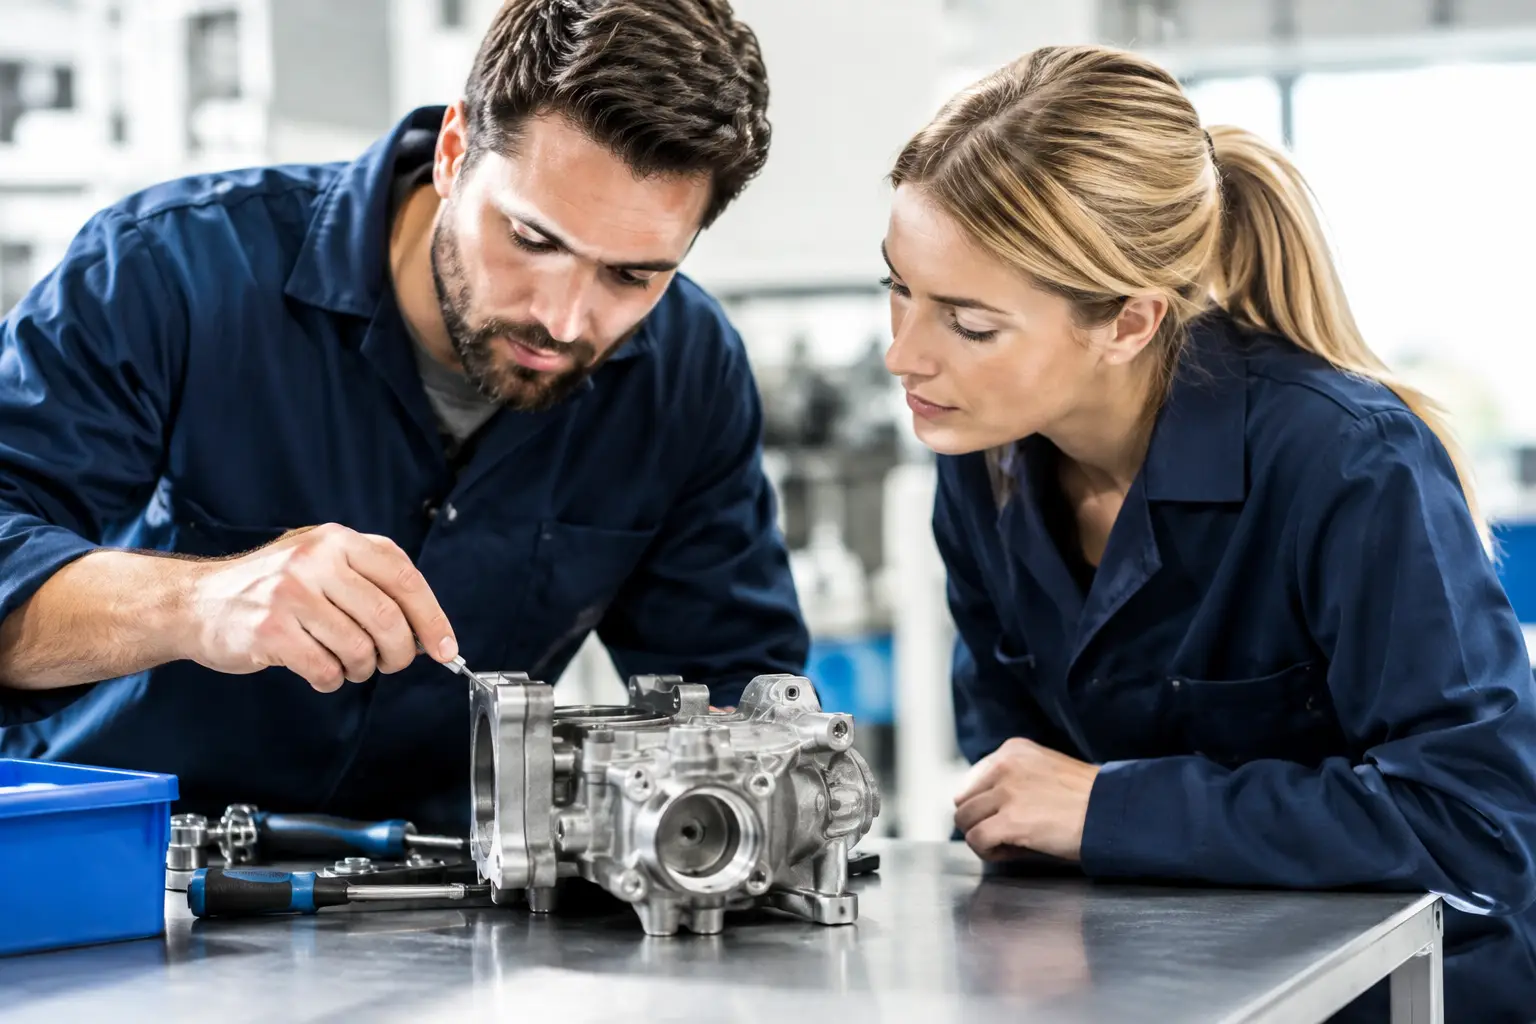
The most effective way to prevent assembly errors is to design the process so that mistakes are difficult to make and easy to detect. End-of-line inspection finds some defects, but it does not recover the time, components or capacity already consumed. Prevention combines clear product data, controlled material flow, suitable fixtures, operator training and fast feedback from every defect.
Identify where errors can occur
Map each assembly step and ask what could be omitted, reversed, mixed, damaged, incorrectly tightened or connected to the wrong location. Use actual defect data, service returns and operator observations. Prioritise failure modes by effect, frequency and detectability. Focus first on errors that affect safety, function or expensive downstream work.
Control the bill of materials and revisions
Operators must receive one approved BOM, drawing set and work instruction. Separate obsolete stock and make engineering changes visible before the next build. Similar-looking variants need distinct identification and storage locations. For outsourced components, a controlled technical drawing handover reduces the chance that incorrect revisions enter assembly.
Present the correct parts in the correct sequence
Kitting works well for complex or variable assemblies because missing parts become visible before work begins. Point-of-use bins can be more efficient for stable high-volume lines. Choose the method based on demand and mix, then define replenishment and shortage escalation. Barcodes, colour coding or shaped locations help distinguish variants, but identifiers should never rely on colour alone where safety or accessibility matters.
Use mistake-proofing at the source
Good mistake-proofing prevents an incorrect action or immediately signals it. Examples include keyed connectors, asymmetric fixtures, component-presence sensors, pick-to-light systems, torque tools with result capture and gauges that accept only the correct orientation. The device must be robust and included in maintenance and calibration. A bypassed sensor creates false confidence.
Make work instructions usable
Instructions should show sequence, tools, settings, critical points and the response to a deviation. Use clear images for orientation or routing, but maintain revision control. Position the instruction where the work happens. Verify competence by observation rather than treating attendance at training as proof.
Check quality before it becomes hidden
Inspect or test features at the point where they are created, especially before covers, potting or later modules make access difficult. Verify torque, sealing, electrical continuity, software configuration or functional movement as appropriate. Record results for critical products and link them to the unit or batch. Our guide to manufacturing supply-chain traceability explains how to maintain this connection.
Control tools, fixtures and measurement
Define tool settings and restrict unauthorised changes. Inspect fixtures for wear and contamination. Calibrate measurement equipment and confirm that the method is repeatable between operators. A correct specification cannot protect quality if the tool applies the wrong force or the gauge gives inconsistent results.
Turn every defect into process learning
Contain the affected scope, identify where the defect was created and where it should have been detected, then remove the cause. Track first-pass yield and repeat defects rather than only final acceptance. Update the risk analysis, instruction or mistake-proofing after verified corrective action. The wider quality framework is covered in quality control for overseas manufacturing.
Preventing errors in outsourced assembly
Agree the BOM, approved process, control plan, test criteria, traceability and change procedure before transfer. Use a pilot build to expose ambiguity and validate fixtures. Monitor defect trends and verify corrective actions on the shop floor. Our practical guide to outsourcing industrial assembly describes these governance controls.
TOS coordinates component sourcing, assembly, inspection and logistics within one programme. This makes responsibility visible and allows design, supplier and process issues to be resolved before they repeat in series production.
Use layered process checks
Supervisors can periodically verify that standard work, tool settings, material identification and mistake-proofing devices remain effective. These short checks are not another final inspection; they confirm that the prevention system is being followed. Record recurring deviations and address the management or process cause instead of reminding operators without changing the conditions.