
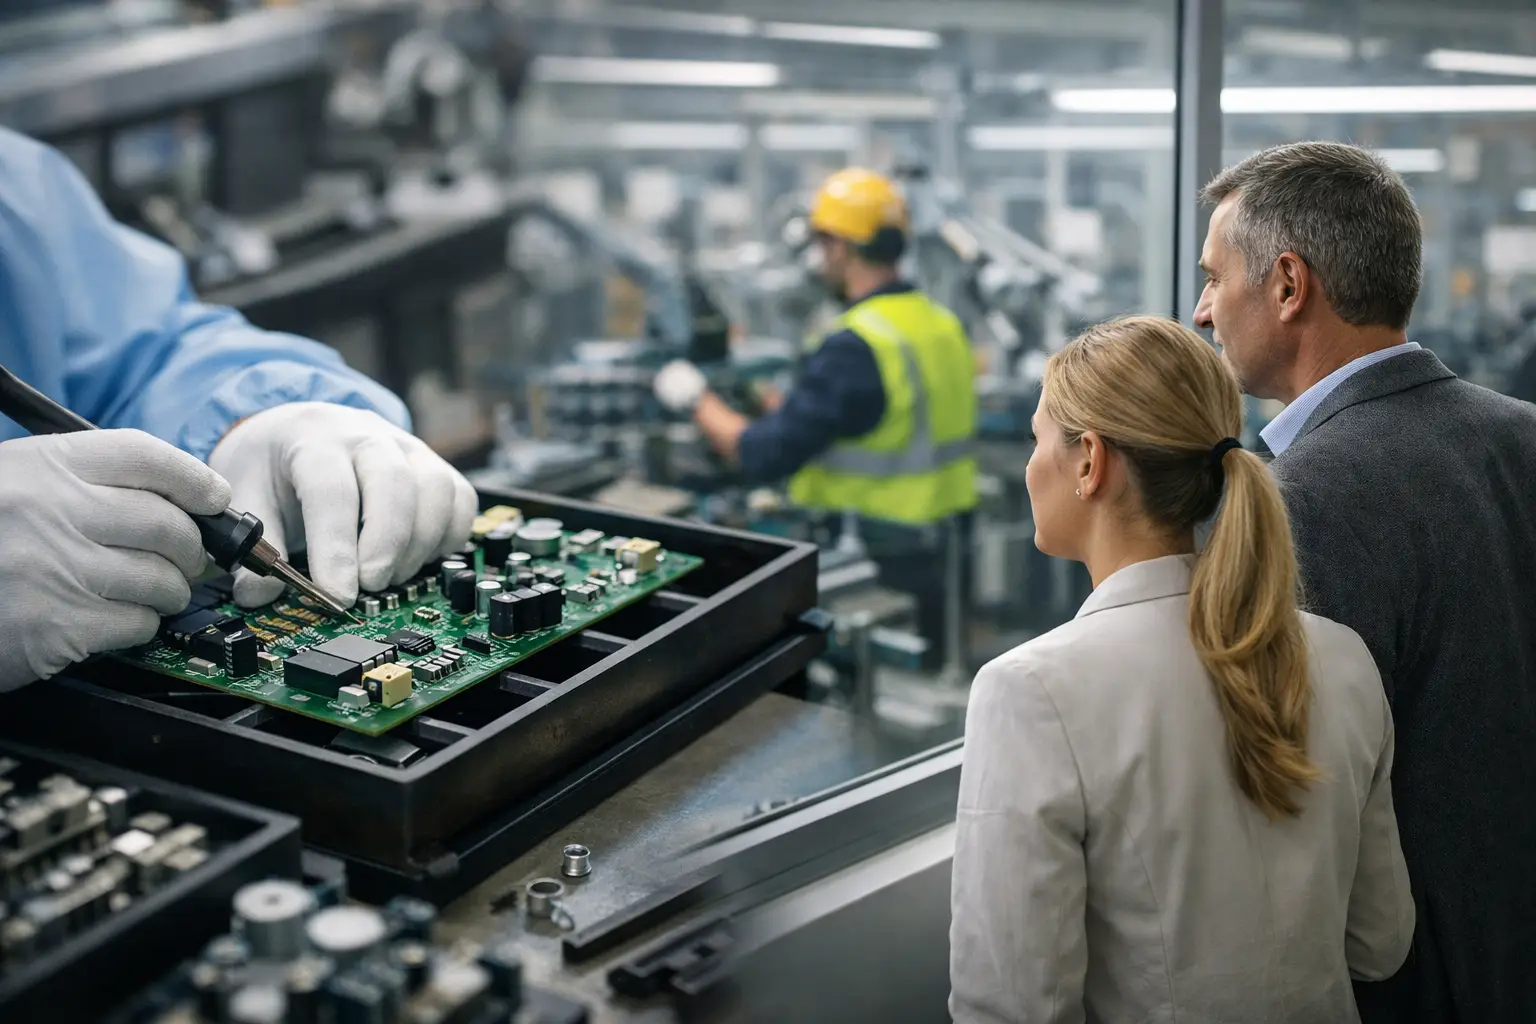
Outsourcing industrial assembly can reduce internal workload, shorten the number of supplier handovers and turn individual components into a tested, ready-to-use module. It can also move quality problems further downstream if bills of materials, work instructions, testing and traceability are not controlled. The decision is therefore not simply whether assembly labour is cheaper elsewhere, but whether the complete process can be specified and verified.
This guide explains the benefits, risks and controls for outsourcing mechanical, electromechanical and technical subassembly work.
What does industrial assembly outsourcing include?
Assembly outsourcing ranges from simple kitting and fastening to complete subassemblies with wiring, electronics, seals, adhesives, software or functional testing. The partner may source components, manufacture custom parts, assemble them and deliver a finished module to your production line.
The scope can include:
- mechanical assembly, fastening and torque control;
- press fitting, bonding, riveting and welding;
- cable routing, connectors and electrical assembly;
- installation of bearings, seals and purchased components;
- labelling, serialisation and packaging;
- visual, dimensional, electrical, pressure or functional testing.
A clear boundary is essential. Define which parts are supplied by you, which are sourced by the assembly partner and who is responsible for shortages, substitutions and incoming inspection.
When does outsourcing industrial assembly make sense?
Outsourcing is attractive when assembly occupies skilled internal capacity without providing a strategic advantage, when demand varies or when coordinating many component suppliers creates too much administrative work. It can also reduce logistics by moving components directly to one assembly location rather than through your own warehouse.
The strongest business case often comes from integration. A partner that coordinates machined parts, sheet metal, plastics and purchased components can solve interface problems before final delivery. This is different from merely moving manual labour: it removes handovers and creates one accountable output.
Consider internal assembly where designs change daily, production knowledge is highly confidential or response time must be almost immediate. A hybrid model is also possible: outsource stable modules while retaining final configuration, software or customer-specific work in-house.
Calculate total landed assembly cost
Compare more than labour rates. Include component sourcing, fixtures, consumables, training, quality control, testing, rejected material, packaging, transport, duties, inventory and the time your own team spends coordinating the process. Include the cost of a line stop if a module arrives incomplete or fails at final installation.
Outsourcing can reduce hidden costs when it consolidates purchasing and inspection. It can also create hidden costs if the supplier is constantly waiting for customer-supplied parts, if engineering changes generate scrap or if every issue requires international expediting. A transparent total-cost model identifies which responsibilities should move with the assembly.
For a structured approach, use the principles in our guide to reducing manufacturing costs through outsourcing.
Freeze the product definition and bill of materials
The assembly partner needs one controlled product definition. The bill of materials should identify every component, revision, quantity, approved manufacturer or specification and allowed alternative. Drawings and CAD data must match the BOM. Software, labels, packaging and consumables should also be included when they form part of the deliverable.
Define effectivity for changes so old and new parts cannot be mixed. The change process should address stock already purchased, work in progress, finished assemblies, fixtures and test programmes. Never rely on an email thread as the only record of an approved substitution.
For assemblies that are not yet production-ready, combine the transfer with engineering and manufacturing support. This helps resolve tolerance stacks, access problems and unclear interfaces before the first batch.
Create visual work instructions and process controls
A drawing shows what the product must become, but it may not show the safest or most repeatable assembly sequence. Develop work instructions with clear steps, photographs or illustrations, tooling, torque values, adhesive requirements, curing time, cleanliness rules and inspection points.
Identify operations that require qualified personnel or validated equipment. Torque tools, crimpers, pressure-test equipment and electrical testers need calibration and maintenance. Adhesives and sealants may require batch control, shelf-life checks and environmental limits.
Use error-proofing where possible. Keyed fixtures, barcode checks, controlled fastener presentation and automated test limits can prevent mistakes rather than detect them later. For manual checks, define exactly what constitutes acceptance and record who completed the operation.
Qualify the assembly partner
Evaluate experience with comparable product complexity, not just available floor space. Review component control, operator training, line layout, electrostatic protection where needed, cleanliness, traceability, testing and non-conformance handling. Confirm how the supplier separates different models and revisions.
Capacity should be assessed at the required takt or batch rate. Ask how the process will respond to demand peaks, absence of trained operators and equipment failures. If the supplier also manufactures components, verify that assembly capacity is not treated as an afterthought behind machine utilisation.
Follow the evidence-based process in our guide to choosing a reliable manufacturing partner. For a complex transfer, an on-site audit and supervised pilot build can reveal practical issues that documents miss.
Validate the assembly with a pilot build
A pilot build tests the documentation, tooling, operator training, component availability and inspection plan under realistic conditions. Use the intended production parts and sequence. Record questions and deviations instead of solving them informally at the workbench.
Compare planned and actual cycle time, identify difficult access, verify ergonomic risks and check whether components can be confused. Confirm that the test method detects deliberately introduced faults where appropriate. The pilot should also validate packaging and labelling.
Approve the pilot only after open issues are incorporated into controlled documents. If an assembly contains high-risk characteristics, use a first-article report or formal validation record before authorising the full series.
Define inspection and functional testing
Final visual inspection alone is rarely sufficient. Build quality into the process with checks after operations that become inaccessible later. Verify critical fasteners, seal placement, connector engagement, polarity, orientation and cleanliness at the point of assembly.
Functional tests should reflect the real failure modes. Depending on the product, this may include continuity, insulation, torque, pressure decay, leakage, movement, force, software response or a simulated operating cycle. Define test limits, equipment, calibration, data retention and the action required after failure.
Trace test results to the assembly or batch when risk requires it. Independent quality control can audit the process and verify shipments, but it should support rather than replace a capable assembly system.
Maintain component and batch traceability
Traceability allows you to isolate risk quickly. Decide which purchased parts require lot, date-code or serial-number records and link them to the finished assembly. At minimum, labels should identify part number, revision, quantity and production batch.
Customer-supplied components need the same discipline. Record receipt, condition, quantity and usage. Agree responsibility for damaged, missing or obsolete parts. A shortage discovered halfway through assembly can disrupt both production and the delivery plan.
When a defect is found, the supplier should be able to identify affected stock, work in progress and shipped assemblies. Containment, root-cause analysis and corrective action must cover both the immediate symptom and the system that allowed it.
Coordinate sourcing, inventory and logistics
An outsourced assembly is only as reliable as its longest-lead component. Build a procurement plan from the BOM, identify single-source items and monitor confirmed dates. Share forecasts so materials can be secured without creating uncontrolled excess inventory.
Agree ownership of raw material, work in progress and finished stock. Define how obsolete components will be handled after an engineering change. Safety stock may be appropriate for critical or long-lead items, but it should be based on a documented risk.
Packaging must protect the completed module and preserve configuration. Include accessories, documents and labels in a final pack-out check. TOS can combine supplier coordination, consolidation and international delivery through its supply-chain service.
Key risks and how to control them
- Wrong revision: use controlled BOMs, effectivity dates and barcode verification.
- Missing components: plan procurement from forecasts and confirm complete kits before build.
- Assembly variation: use visual instructions, fixtures, training and in-process checks.
- Undetected functional faults: validate test methods against real failure modes.
- Loss of traceability: link component lots and test data to batches or serial numbers.
- Damage in transit: validate packaging with the final module and transport route.
- Supplier dependency: retain product data, tooling rights and a documented transfer plan.
Industrial assembly outsourcing checklist
- Define the scope and responsibility for every component.
- Release one controlled BOM, drawing set and revision.
- Create repeatable work instructions and calibrated controls.
- Qualify the partner for the actual assembly complexity.
- Run and document a pilot build.
- Verify critical operations before they become inaccessible.
- Validate functional testing and retain appropriate records.
- Plan materials, traceability, packaging and change control.
Outsource assembly without losing product control
Assembly outsourcing is valuable when it transfers a complete, controlled process rather than a collection of loose tasks. The partner must understand what to build, how to verify it and how to respond when a component or result differs from the specification.
TOS helps industrial companies combine custom-part manufacturing, component sourcing, assembly, quality control and delivery under one point of coordination. Share your BOM, drawings, expected volumes and test requirements through our contact page to evaluate a suitable assembly route.